Socket Weld vs Butt Weld: SW/BW on Japanese Piping Specs
The piping class from your Japanese EPC contractor or equipment supplier lists small lines as "SW" and larger lines as "BW," and the valve list uses the same two letters. Order a 25A valve with the wrong end, and it arrives on site and cannot be joined to the pipe.
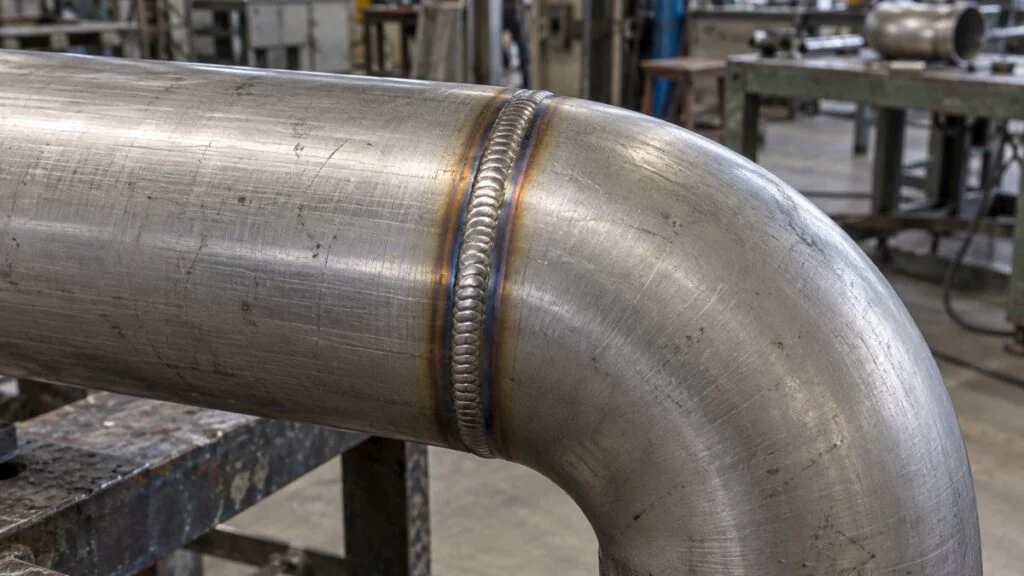
The short answer: SW is a socket weld. The pipe slides into a socket on the fitting or valve, and a fillet weld is laid around the outside. BW is a butt weld. Two beveled ends are placed end to end and the groove between them is filled with weld metal. In Japanese practice, SW is typical at 50A (NPS 2) and below and BW at 65A (NPS 2-1/2) and above. That split is a working rule of thumb, not a limit in the standards, and BW is also used on small lines when strength or service conditions call for it.
This guide explains what the two letters mean on Japanese documents, why size is the usual dividing line, how valve ends differ, and what to check before you order. It ends with a checklist, questions for the Japanese side, and a sample inquiry email.
An SW joint is inserted and welded on the outside. A BW joint brings two beveled ends together and fills the groove.
Blue: weld. Dark gray: pipe. Light gray: fitting. Schematic, not to scale.
Contents
- What SW and BW Mean on Japanese Piping Documents
- Why Size Usually Decides: SW at 50A and Below, BW at 65A and Up
- How SW and BW Valve Ends Differ
- Socket Weld vs. Butt Weld: Side-by-Side Comparison
- The 1/16-Inch Gap and Crevice Corrosion in Socket Welds
- Checklist Before You Order SW or BW Fittings and Valves
- Questions for the Japanese Side
- Limits of This Guide
- FAQ
- Sources
What SW and BW Mean on Japanese Piping Documents
Japanese piping specs, valve lists, and fitting orders use the English abbreviations, often next to the Japanese names:
- SW (socket weld): 差込み溶接 (sashikomi yosetsu), literally "insert welding." JIS calls these fittings the socket-welding type.
- BW (butt weld): 突合せ溶接 (tsukiawase yosetsu), literally "butt-together welding." The katakana バットウェルド (batto werudo) is closest to the English, but バッドウェルド (baddo werudo) is also widely used on the shop floor and in documents. Both mean BW.
- Bevel: 開先 (kaisaki), the angled edge machined on a BW end.
Sizes come in the JIS "A" (millimeter-based) designation, with the inch-based "B" designation sometimes alongside. 50A equals 2B, which is NPS 2. Do not read 50A as an outside diameter. For how JIS sizes and wall schedules line up with ASME, see our JIS pipe schedule and thickness chart.
One trap: on electrical drawings, "SW" usually means a switch. Read the letters in the context of the drawing type.
Why Size Usually Decides: SW at 50A and Below, BW at 65A and Up
On small lines, a butt weld has a drawback. Any weld bead that pushes through to the inside of the pipe takes up a larger share of the bore as the pipe gets smaller. That raises the risk of blockage or disturbed flow. A socket weld keeps the weld on the outside.
SW is also easier to fit up in the field. Pushing the pipe into the socket centers it automatically, while a small-bore butt weld needs the two pipes carefully aligned end to end. A butt weld, however, makes the stronger joint, so designers switch to BW even on small lines when conditions demand it.
Expect BW on small-bore lines in services like these:
- High pressure or high temperature, where the weld must be strong
- Vibration or repeated swings in pressure or temperature
- Fluids that cause crevice corrosion or erosion (wear from the flow itself)
- Food and pharmaceutical lines, where crevices are not acceptable
- Lines where the weld must be inspected through its full thickness
The 50A line is not a standard limit. ASME B16.11, the US standard for socket-welding fittings, gives dimensions up to NPS 4 (100A). The process piping code ASME B31.3, however, does not permit socket welds larger than DN 50 (NPS 2) in severe cyclic conditions. That rule is one reason 50A so often becomes the cutoff.
Start with the size, then switch small lines to BW when the service calls for it.
On Japanese projects, that rule lives in the 配管仕様書 (haikan shiyosho), the piping specification or piping class. Each line on the P&ID carries a spec code that points to it. If you are new to the Japanese drawing set, our guide to PFDs and P&IDs on Japanese projects explains how those drawings fit together.
How SW and BW Valve Ends Differ
Many valves are offered with either end, and the choice changes the shape of the connection. The ball valve sketch below shows the difference.
An SW end has a recessed socket. A BW end is beveled to match the pipe wall.
Blue: weld. Dark gray: pipe. Light gray: valve. Schematic only; actual body shapes vary by maker.
An SW end is a recessed socket that the pipe slides into. A BW end is machined to the same wall as the pipe, with an angled bevel at the tip. ASME B16.25, the standard for butt-welding ends, specifies a single-V bevel angle of 37.5° (a 75° included angle) for typical wall thicknesses.
Either way, the bore is close to the pipe bore after welding. But SW and BW ends are not interchangeable, and a valve with the wrong end cannot be joined to the line. Confirm the end type before you place a valve order.
Fittings and valves are named by end type plus fitting type, so a "BW elbow" is a butt-welding elbow and an "SW tee" is a socket-welding tee.
The end type comes first in the name. A BW elbow is a butt-welding elbow.
An SW 90° elbow and a BW 90° elbow have different ends and are not interchangeable.
For flanged ends, JIS and ASME flanges do not bolt together directly. See JIS vs. ASME (ANSI) vs. JPI flanges and flat face vs. raised face flanges.
Socket Weld vs. Butt Weld: Side-by-Side Comparison
Size, bore condition, fit-up, and inspection decide which joint suits a line.
"Weld strength" compares the same size and wall thickness as a general tendency. Actual strength depends on design conditions, workmanship, and inspection.
Inspection often settles the choice. The shape of a fillet weld makes it hard to radiograph, so socket welds are usually checked at the surface. When a line needs its welds checked through the full thickness, designers pick BW.
The 1/16-Inch Gap and Crevice Corrosion in Socket Welds
Socket welds have one fit-up rule that matters in every review. The pipe is pushed in until it bottoms out in the socket, then pulled back about 1.6 mm (1/16 in.) before welding. If the pipe stays bottomed out, weld shrinkage or thermal expansion in service can push the pipe against the bottom of the socket and crack the weld.
Codes such as ASME B31.1 and B31.3 require this gap before welding. The B31.3 figure shows it as approximately 1.5 mm (1/16 in.).
Backing the pipe out slightly leaves room for expansion and shrinkage.
The ASME B31.3 figure shows approximately 1.5 mm (1/16 in.) before welding. It does not specify the gap after welding.
That gap stays in the joint after welding, and fluid can sit in it and cause crevice corrosion. Stainless steel is not immune. Crevices are one of the places where local corrosion starts on grades such as SUS304 (comparable to AISI 304).
Related: SUS304, SUS316, SUS430: JIS Grades and AISI/ASTM Equivalents
ASME B31.3 also says socket welds should be avoided in services where crevice corrosion or severe erosion may occur. For corrosive fluids and for food or pharmaceutical lines that cannot tolerate crevices, BW is the choice even at small sizes.
Checklist Before You Order SW or BW Fittings and Valves
A mix-up between SW and BW usually shows up on site, when the pipe will not join the valve. Check these items against the piping class before you order:
- End type: SW, BW, flanged, or threaded, for every valve and fitting on the line
- Size and wall: for BW, match the fitting wall to the pipe schedule (Sch). For SW, pick the fitting's wall category: Sch 80 or Sch 160 under JIS B 2316, or Class 3000, 6000, and so on under ASME B16.11
- Material: carbon steel, stainless, or other, matched between pipe and fittings
- Standard: JIS or ASME. Names can look the same while dimensions differ. JIS and ASME pipe ODs are not always equal, so check that fittings and pipe come from the same system
- Pipe making process, if the spec calls for it: seamless or ERW. See JIS ERW vs. seamless pipe codes
- Scope at equipment nozzles: when a valve connects to a flange on a piece of equipment, confirm who supplies the mating (companion) flange and settle the end type early
Order formats vary by company. A typical Japanese order line puts the end type, fitting type, size, wall, material, and standard on one line, for example:
BW 90° long elbow 50A Sch 40 SUS304 JIS B 2312
That reads as a butt-welding, 90-degree, long-radius elbow, nominal size 50A (NPS 2), schedule 40 wall, SUS304 stainless, to JIS B 2312. Writing all six items on every line is the simplest way to avoid mix-ups. Reducers follow the same pattern.
Questions for the Japanese Side
- Which piping class applies to this line, and at what size does it change from SW to BW?
- Which fitting standard applies: JIS B 2316 or B 2312, or ASME B16.11 or B16.9? Which standard are the valve ends made to?
- Are the pipe ODs to JIS or to ASME? Are socket bores and bevels made for the same OD?
- For SW fittings, which wall category: Sch 80 or Sch 160 (JIS), or Class 3000 or 6000 (ASME)?
- For BW ends, which bevel standard and which pipe schedule should the ends match?
- Does any small-bore line use BW because of pressure, cyclic loading, corrosion, sanitary service, or inspection requirements?
- What weld inspection is required on SW and BW joints (visual, PT, MT, RT, UT)?
A short inquiry you can adapt:
Subject: End connections for valves on line [line number]
Hello [name],
Before we place the valve order, please confirm the end connections for line [line number] (piping class [code]). We read the class as SW for 50A and below and BW for 65A and above. Is that correct for this line? Please also confirm the fitting standard (JIS or ASME), the SW wall category (Sch 80/160 or Class 3000/6000), and the pipe schedule the BW ends should match.
Best regards,
[your name]
Limits of This Guide
- The 50A/65A split is a common rule of thumb in Japan, not a requirement in JIS or ASME. The project piping class decides.
- Code references here are summaries. Use the edition of ASME B31.1 or B31.3 (or the Japanese code) that applies to your project, and leave design decisions to the responsible piping engineer.
- The fit-up gap and inspection notes describe what to check, not a welding procedure. Follow the qualified procedure for your job.
- Company order formats and terms vary. The order line above is an illustration.
FAQ
What Does SW Mean in Piping?
SW means socket weld. On Japanese piping specs and valve lists it marks a socket-welding end, called sashikomi yosetsu in Japanese. The JIS standard for steel socket-welding pipe fittings is JIS B 2316. On electrical drawings, SW usually means a switch instead.
What Is a BW Elbow?
A BW elbow is a butt-welding elbow. Both ends are beveled and butt-welded to the pipe. Dimensions are set by JIS B 2312 or ASME B16.9, and they come in long-radius and short-radius versions.
Why Not Use Socket Welds Above NPS 2?
Socket welds above NPS 2 are allowed in many services, and ASME B16.11 covers fittings up to NPS 4. But ASME B31.3 does not permit them above DN 50 (NPS 2) in severe cyclic conditions, BW is stronger and easier to inspect, and fewer SW fitting sizes are on the market. That is why many piping classes switch to BW at about that size.
What Is the Difference Between Socket Weld and Threaded Fittings?
Both are used on small lines. Threaded fittings screw together with pipe threads, so they need no welding and can be taken apart. Socket welds are fixed by welding, so they leak less and suit high-temperature, high-pressure lines and fluids where leaks are not acceptable.
Sources
- Japanese Standards Association, JIS B 2316:2017 Steel socket-welding pipe fittings, preview (Japanese)
- Japanese Standards Association, JIS B 2312:2024 Steel butt-welding pipe fittings, preview (Japanese)
- ASME, B16.11 Forged Fittings, Socket-Welding and Threaded
- ASME, B16.9 Factory-Made Wrought Buttwelding Fittings
- ASME B16.11 size range: Project Materials, "What Is ASME B16.11?"; Ferrobend, "ASME B16.11 Socket Weld Class 3000 Coupling Dimensions"
- ASME B16.25 bevel: Project Materials, "What Is Pipe Beveling?"
- Socket weld gap (ASME B31.1 and others) and why it is needed: EPRI, "Analysis of Socket Welded Assembly Gap" (1009715); A Marine Blog, "Why Is the Gap Needed on Socket Welds"
- ASME B31.3 limits on socket welds: Little P.Eng., "ASME B31.3 Limitations on Welded Joints"
- JIS B 2316 wall categories: SVF, stainless socket-welding fittings to JIS B 2316, Sch 80 and Sch 160 (Japanese)
- Inspection of fillet vs. butt welds: Project Materials, "Fillet Weld vs Butt Weld"
Original article in JapaneseThis guide is adapted from a MONOSCOPE article written for readers in Japan: SW(ソケットウェルド)とBW(バットウェルド)の違いと使い分け|配管の溶接継手
About the editor
 MONOSCOPE EditorFOUNDER & EDITOR
Spent about ten years at a plant equipment maker and a plant engineering company, proposing, designing, and commissioning equipment, then moved into web marketing. Now a web consultant for B2B manufacturers, helping them explain their products and technology. Licensed in Japan as an Energy Manager and a Third-Class Chief Electrical Engineer.
Has run an engineering blog since 2017 (500+ articles) and a Japanese YouTube channel with about 20,000 subscribers. Each English guide is written from the Japanese shop-floor point of view and checked against the cited standards.